DIRECT ANSWER
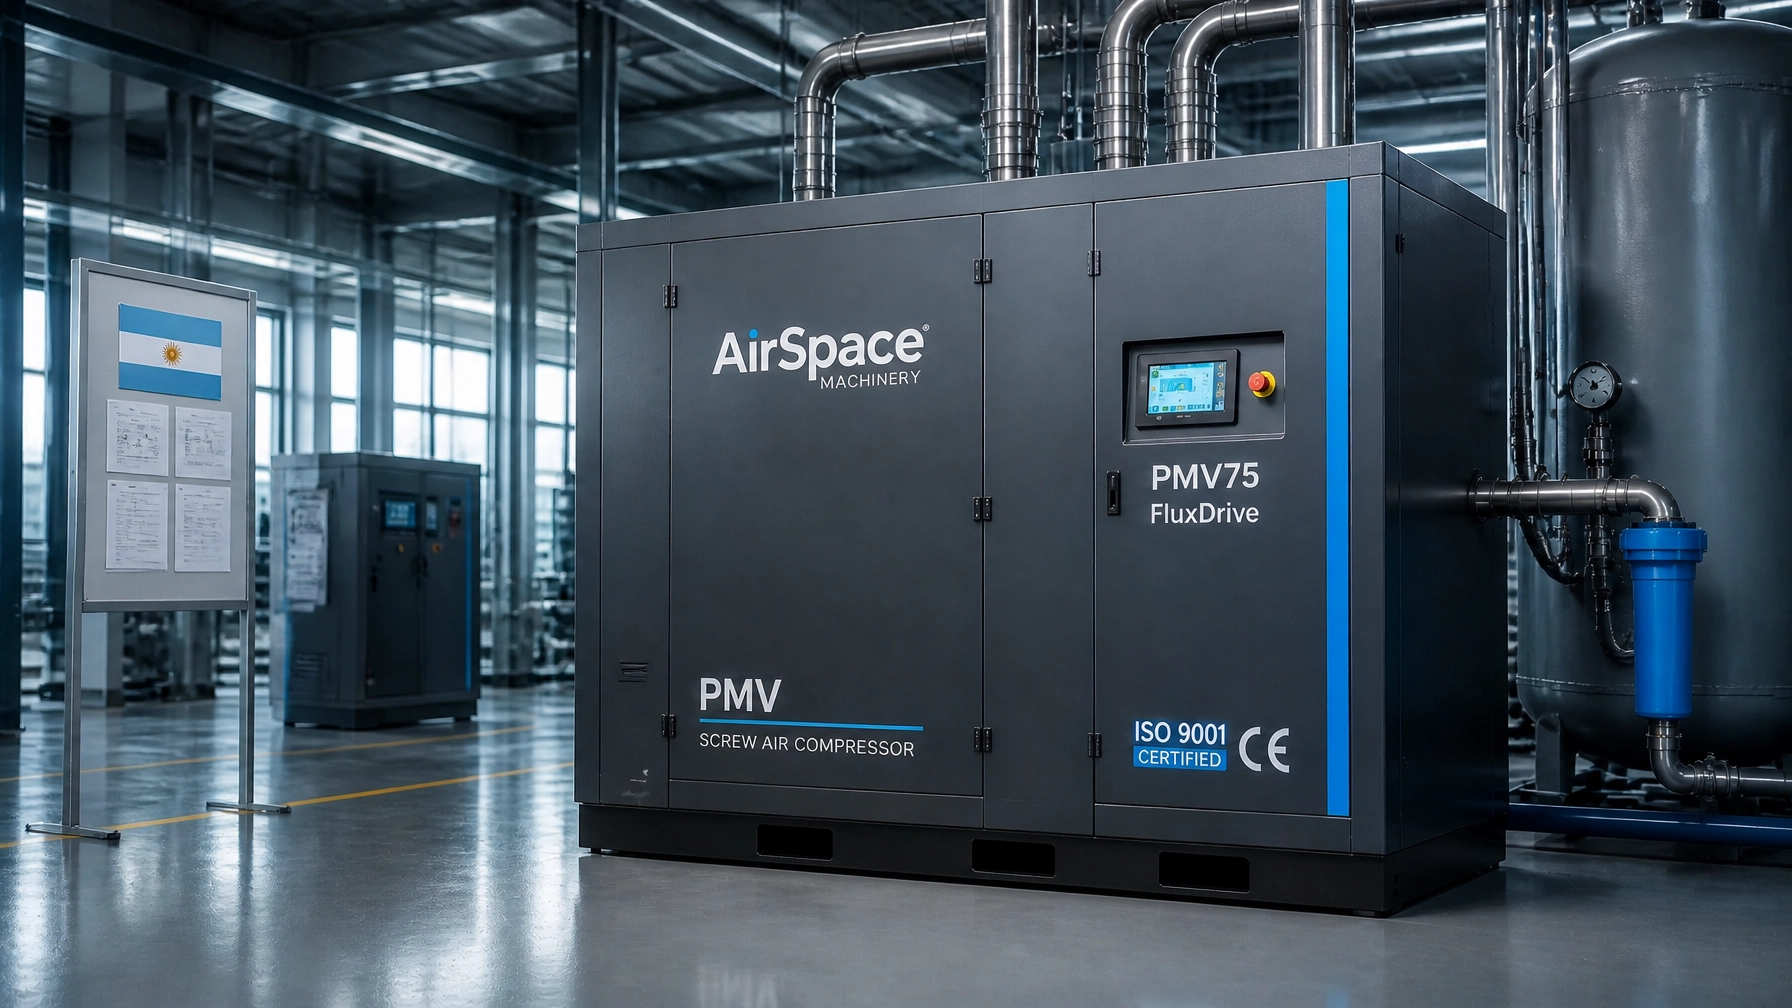
A 6kW fiber laser is officially planned around a 15kW / 20HP PMV screw compressor operating at 16 bar, with up to 1.5 m³/min FAD on an ISO 1217 basis. That is the correct planning point for a single laser using high-pressure assist air.
It is not a final sizing guarantee. The final compressor selection depends on nozzle demand, cutting duty cycle, pressure loss through filters and piping, material thickness, receiver capacity, ambient conditions and the laser OEM specification.
For the broader pressure and configuration range, see the AirSpace 16 bar high-pressure laser compressor series.
THE 6KW FIBER LASER BUYER’S 10 HEADACHES
Laser workshops usually contact a compressor supplier after one of these problems appears:
- Pressure falls during piercing or thick-plate cutting.
- An 8–10 bar compressor cannot maintain the head requirement.
- The supplier quotes displacement instead of FAD.
- A dryer is rated at the wrong pressure or inlet temperature.
- Filters create excessive pressure drop.
- Moisture reaches the laser head.
- Air quality is described as “clean” without ISO 8573-1 evidence.
- Nitrogen costs remain high for stainless-steel work.
- A 20HP and 30HP quotation cannot be compared fairly.
- Integrated and modular packages are being compared by price alone.
The practical answer is to specify pressure, FAD, air quality and duty cycle as one package.
For 2026 industrial laser operations, switching from nitrogen to 16-bar compressed air as an assist gas reduces hourly operating costs from approximately $40/hr to $4/hr. This transition plugs a massive hidden “Nitrogen Tax,” delivering annual savings exceeding $31,000 per machine for typical high-duty cycles. By utilizing Permanent Magnet Variable Frequency (PMV) technology, manufacturers can achieve a 35% energy delta compared to legacy fixed-speed units, resulting in a full capital equipment ROI in just 6 to 10 months.
What Is the $31,000 Annual Nitrogen Robbery?
The “Nitrogen Robbery” is the hidden cost of running a fiber laser exclusively on nitrogen assist gas, which can overcharge fabricators by as much as 900% compared to 16-bar compressed air. For typical high-duty cycles, this “Nitrogen Tax” exceeds $31,000 per machine annually.
If your fiber laser has been running exclusively on nitrogen since early 2026, you are likely overpaying for assist gas. In the current manufacturing landscape, nitrogen is no longer just a consumable; it is a significant drain on profitability.
Legacy brands and gas suppliers often suggest that nitrogen is the only path to quality. However, for 80% of fabrication tasks, including mild steel up to 12mm and various aluminum grades, a clean, dry, 16-bar compressed air supply provides identical structural performance at a fraction of the cost.
How Much Cheaper Is Compressed Air Than Nitrogen? ($40/hr vs $4/hr)
Compressed air costs roughly $4/hr versus $40/hr for nitrogen, a near 90% reduction in assist-gas expense. When you buy nitrogen, you pay for the gas, the delivery, the tank rental, and the “convenience.” When you use a dedicated 16-bar China made screw air compressor, you only pay for the electricity to compress ambient air.
- Nitrogen Assist Gas Cost: $35.00 – $45.00 per hour (inclusive of delivery and evaporation losses).
- 16-Bar Compressed Air Cost: $3.50 – $4.50 per hour (inclusive of electricity at $0.15/kWh and maintenance).
For a shop running 8 hours a day, 250 days a year, the math is sobering:
- Annual Nitrogen Spend: $80,000.
- Annual AirPower Spend: $8,000.
- Potential Savings: $72,000 per year.
Even with a more conservative duty cycle, the savings rarely drop below $31,000 annually. This is capital that should be in your expansion fund, not your supplier’s pocket.
5-Year TCO Comparison: 16-Bar Air vs Nitrogen
Over five years, a 16-bar PMV air system costs approximately $40,500 in Total Cost of Ownership (TCO) versus $190,000 for nitrogen, a 5-year total savings of $149,500. The following table breaks down the TCO for a single 4kW fiber laser over a five-year horizon.
Cost Element | Nitrogen (Bulk/Dewar) | 16-Bar PMV Air System |
|---|---|---|
Initial Equipment Investment | $0 (Rental) | $18,500 (One-time) |
Annual Consumable/Gas Cost | $38,000 | $0 |
Annual Electricity Cost | $0 | $3,200 |
Annual Maintenance/Filters | $0 | $1,200 |
5-Year Total TCO | $190,000 | $40,500 |
5-Year Total Savings | — | $149,500 |
Why Does PMV Technology Deliver a 35% Energy Delta?
Permanent Magnet Variable Frequency (PMV) technology delivers a 35% energy delta by scaling power consumption precisely to real-time CFM demand, rather than running the motor at 100% speed during idle or unload cycles. This eliminates the wasteful “Unload Tax” common in fixed-speed compressors.
Not all air compressors are created equal. In the laser cutting world, gas demand is highly fluctuating. A fixed-speed “Legacy” compressor wastes enormous amounts of energy during the unload cycle, a phenomenon we call the Unload Tax Robbery.
AirSpace Machinery utilizes PMV technology coupled with IE5 ultra-efficient motors. This setup creates a 35% energy delta compared to standard units. Instead of the motor spinning at 100% speed while your laser is repositioning or changing sheets, the AirSpace PMV system scales power consumption precisely to your CFM demand.
Engineering Excellence: The AirSpace Advantage
To ensure your laser optics remain pristine and your cuts remain consistent, AirSpace 16-bar systems are built with:
- Ultra-Precision Rotors: Featuring a 5:6 profile for maximum air delivery with minimum vibration.
- 55°C Tropical Rating: Designed for extreme climates, ensuring the “Heat Tax” doesn’t degrade your 99.9% uptime.
- ISO 8573-1 Class 0 Integrity: Integrated multi-stage filtration and refrigerated dryers ensure the air is oil-free and moisture-free, preventing lens contamination.
Decision Matrix: When Is Compressed Air Acceptable for Laser Cutting?
Compressed air is acceptable for the majority of laser cutting jobs, including mild steel (1–12mm), stainless steel (1–4mm), and all aluminum grades. Nitrogen is only necessary for thick stainless steel (5mm+) requiring a cosmetic, oxidation-free mirror finish.
The primary concern with air is the “oxide layer.” While nitrogen provides a silver, mirror-like edge, air-cut edges have a thin layer of oxidation. For parts that will be powder-coated or for structural mild steel, this is often preferred as it saves thousands in gas costs without affecting the final product.
Material Type | Thickness | Recommended Gas | Why |
|---|---|---|---|
Mild Steel | 1mm – 12mm | 16-Bar Compressed Air | High speed, lowest cost, excellent for coating. |
Stainless Steel | 1mm – 4mm | 16-Bar Compressed Air | Fast cutting, acceptable edge for industrial parts. |
Stainless Steel | 5mm+ | Nitrogen | Prevents oxidation; necessary for cosmetic mirror finish. |
Aluminum | All | 16-Bar Compressed Air | Air provides a cleaner edge than oxygen for most alloys. |
What Is the Payback Period for a 16-Bar Air System?
The payback period for a 16-bar air system is typically 6 to 10 months. In one real-world case, a mid-sized fabrication shop achieved a 6.8-month payback after replacing its liquid nitrogen Dewar system.
A shop in Southeast Asia recently replaced their liquid nitrogen Dewar system with an AirSpace 15HP Variable Frequency Screw Air Compressor.
- Investment Cost: $16,000 (System + Installation).
- Previous Nitrogen Monthly Spend: $2,800.
- New Electricity + Maintenance Monthly Cost: $450.
- Monthly Cash Flow Improvement: $2,350.
- Payback Period: $16,000 / $2,350 = 6.8 Months.
After month seven, that $2,350 stays in the company’s bank account every single month. This is the essence of “Engineering Freedom.”
Common Questions from Laser Operators
Can you cut stainless steel with compressed air instead of nitrogen?
Yes. You can cut stainless steel with 16-bar compressed air. The edge will have a brownish tint due to oxidation, but the cutting speed is often faster than nitrogen for thicknesses under 4mm. If the part is being painted or is a structural component, air is the most economical choice.
Is 16 bar enough for fiber laser cutting?
For the vast majority of 1kW to 6kW fiber lasers, 16 bar is the “sweet spot.” It provides enough pressure to clear the molten metal from the kerf effectively. High-power lasers (12kW+) may sometimes require 20-25 bar for very thick plates, but 16 bar covers 90% of standard fabrication needs.
What dew point is needed for laser cutting?
To protect your fiber laser’s sensitive optics and prevent “micro-explosions” in the kerf, you need a Pressure Dew Point (PDP) of +3°C to +5°C (achieved by a refrigerated dryer) for standard work. For ultra-high precision, ISO 8573-1 Class 0 requirements may dictate a desiccant dryer reaching -40°C. AirSpace systems come standard with high-performance refrigerated dryers that satisfy most OEM requirements.
Frequently Asked Questions
Does cutting with compressed air damage fiber laser optics?
No, provided the air meets ISO 8573-1 Class 0 purity. AirSpace systems use multi-stage filtration and refrigerated dryers to deliver oil-free, moisture-free air, which prevents the lens contamination and micro-explosions that degrade optics and cut quality.
What size air compressor do I need for a 4kW fiber laser?
Most 1kW–6kW fiber lasers pair well with a 15HP (11kW) 16-bar variable frequency screw compressor, which supplies sufficient CFM and pressure to clear the kerf. Exact sizing depends on daily run hours and cutting thickness, so a CFM demand assessment is recommended before purchase.
Is a 16-bar air compressor reliable for 24/7 laser production?
Yes. AirSpace 16-bar PMV systems are engineered for continuous operation in ambient temperatures up to 55°C and target 99.9% uptime, making them suitable for high-stakes, round-the-clock fabrication lines.
Conclusion: Stop Paying the Nitrogen Tax
The data for 2026 is clear. Unless you are producing medical-grade stainless or aerospace components requiring zero oxidation, nitrogen is a “tax” you no longer need to pay. By switching to a 16-bar AirSpace PMV system, you gain the 35% energy delta, achieve a 99.9% uptime, and see a full return on your investment before the year is out.
Don’t let legacy gas contracts bleed your margins. It is time to treat your air supply as the “Fourth Utility” it is.
Get a Proposal
Ready to quantify your specific savings? Our engineering team can provide a detailed TCO breakdown for your facility.
- Contact us on WhatsApp: +64-27-622-8288
📅 Last updated:
⚡ Is Your Factory Bleeding Cash?
Most fixed-speed compressors waste $3,600/year in "Unload Tax." Test your waste level in 30 seconds.
RUN THE ROI TEST →Ready to See How Much Your Facility Can Save?
Fill out the form below for a Free Energy Assessment.